Is Your Container Ready?
Get In Contact With Us Today
Is Your Container Ready?
Get In Contact With Us Today
2026 Top Chromium Carbide Wear Plate Suppliers
Mining, cement, steel, and recycling plants face relentless abrasion in 2026. Conveyor chutes groan. Hoppers lose thickness. Downtime becomes expensive quickly.
This guide evaluates leading chromium carbide wear plate suppliers through practical performance, not marketing claims. Key factors include deposit chemistry, carbide distribution, base-plate toughness, welding quality, dimensional accuracy, and delivery consistency. Field experience matters. A plate that survives a laboratory test may still crack beside a weld or deform under impact. That weakness deserves attention.
The U.S. Geological Survey’s Mineral Commodity Summaries 2025 highlights chromium’s importance in alloy production and stainless steel manufacturing. Its findings support a broader reality: chromium supply influences material pricing, availability, and purchasing risk. Meanwhile, ASTM G65 remains a widely used laboratory method for comparing abrasive wear resistance. It cannot reproduce every mine site. No test can.
Tribologist J.F. Archard stated, “The volume of wear is proportional to the load and sliding distance.” His principle remains useful when engineers estimate liner life and replacement intervals. However, carbide hardness alone does not guarantee reliable service. Plate thickness, dilution, heat input, impact conditions, and installation practice also matter.
Our 2026 supplier overview combines technical documentation, production evidence, customer experience, and reported quality controls. We examine whether suppliers disclose chemistry, hardness ranges, overlay patterns, and inspection procedures. Some claims appear impressive. Some need stronger proof. That distinction is important.
The best supplier is not always the cheapest. It is the one that delivers predictable protection, practical support, and honest limitations. That is where this review begins.
Chromium Carbide Wear Plates: 20–35% Cr, 55–65 HRC, and Core Uses
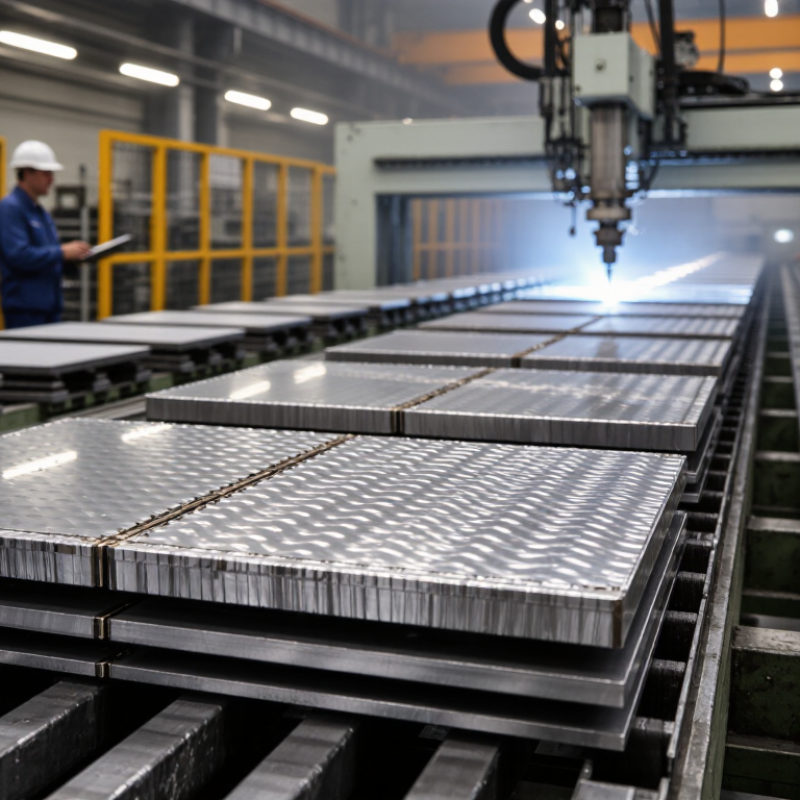
Chromium carbide wear plates are designed for severe abrasion, not decorative toughness. Their overlay commonly contains 20–35% chromium carbides in a welded matrix. Hardness often reaches 55–65 HRC. These figures matter, but they do not tell the whole story. In quarry chutes, transfer points, cement mills, and coal-handling liners, sliding rock can remove steel quickly. I have seen a hard plate fail early because its weld pattern was uneven. That detail is easy to miss.
Reliable suppliers should provide traceable chemistry, overlay thickness, base-plate grade, and hardness test results. Ask how the plate was welded and whether surface cracks are controlled. Fine, evenly distributed cracks can relieve welding stress. Large, deep cracks may signal poor process control. Plate flatness also affects installation, especially around curved hoppers and vibrating screens. A supplier with practical fabrication guidance is often more useful than one offering impressive numbers alone.
Tips: Match plate hardness to the actual wear mode. Impact requires toughness, while sliding abrasion favors a hard overlay. Use recommended cutting methods, and avoid drilling through the carbide layer when possible. Check corners and bolt holes during inspection. Laboratory data can look perfect, yet field conditions remain less predictable.
2026 Top Chromium Carbide Wear Plate Suppliers — Chromium Carbide Wear Plates: 20–35% Cr, 55–65 HRC, and Core Uses
Typical chromium carbide overlay wear plates combine a chromium-rich carbide layer with a mild-steel backing plate. The chart shows commonly specified composition and hardness ranges; actual values vary by manufacturing process and product grade.
How 2026 Suppliers Manufacture Overlays with 30–50% Carbide Content
Leading chromium carbide wear plate suppliers usually target 30–50% carbide content in the overlay. This figure normally means carbide volume fraction, not total alloy weight. ASM Handbook, Volume 18, reports that chromium-rich carbides form within an iron-based matrix during hardfacing. The matrix absorbs impact, while angular M7C3 carbides resist cutting abrasion. The balance matters. Too little carbide shortens service life. Too much can increase cracking.
MANUFACTURING Manufacturing starts with a low-carbon steel plate, cleaned by blasting and checked for flatness. Suppliers then deposit Fe-Cr-C wire or powder through open-arc, submerged-arc, or cored-wire welding. Controlled heat input limits dilution from the base plate.
A typical overlay may receive one or two passes, producing a layer about 3–12 millimeters thick. Cooling is deliberately slow. Rapid cooling can create visible stress cracks.
Small cracks are often acceptable, but wide or connected cracks need investigation.
According to the 2025 USGS Mineral Commodity Summaries, global chromite mine output reached roughly 41 million metric tons in 2024. Stable chromium supply supports consistent alloy formulation, though raw material quality still varies. ISO 14700:2017 emphasizes classification and testing of hardfacing consumables, while ASTM G65 remains widely used for abrasive wear comparison. In practice, I would request carbide-volume measurements, hardness mapping, and test coupons from every batch. Supplier claims can sound precise. Production is less perfect.
Comparing Suppliers by ASTM G65 Abrasion Testing and EN 10204 3.1 Reports
2026 Top Chromium Carbide Wear Plate Suppliers: Comparing Suppliers by ASTM G65 Abrasion Testing and EN 10204 3.1 Reports
A credible supplier should provide ASTM G65 abrasion results for the actual plate grade. The report should identify the test procedure, specimen thickness, abrasive type, wheel condition, and mass loss. These details matter. A low wear value means little when testing conditions remain unclear.
During supplier reviews, request samples from the same production batch. Compare carbide distribution under magnification, overlay hardness, crack patterns, and weld quality. ASTM G65 measures abrasive wear, not impact resistance, edge cracking, or field welding performance. That limitation is easy to overlook. I have seen plates with impressive hardness data perform poorly where large rocks strike at an angle.
An EN 10204 3.1 certificate adds traceability and technical confidence. It should connect the plate to a heat number, chemical composition, dimensions, delivery condition, and recorded test results. The document must be issued by the manufacturer’s authorized inspection representative, not copied from a previous order. Check whether the certificate matches the plate markings and packing list.
Supplier comparisons should combine both records, not rank companies by one impressive number. Ask how samples were prepared and whether results came from production plates or laboratory coupons. Some certificates look complete but omit test standards or acceptance criteria. That is a warning sign. Independent verification can strengthen the review, although it adds time and cost. No test fully predicts service life. Field feedback still matters.
Assessing Plate Thickness, Overlay Hardness, Welding Methods, and ISO 9001
When evaluating 2026 chromium carbide wear plate suppliers, plate thickness should match the equipment’s actual wear pattern. A 10 mm plate may suit moderate abrasion, while a 20 mm plate can reduce replacement frequency in severe service. However, thicker is not always better. It may increase weight, welding difficulty, and structural stress. Ask for measured thickness, not only nominal values.
Overlay hardness deserves careful review. Many plates fall near 55–65 HRC, but hardness alone cannot predict service life. The carbide distribution, matrix structure, crack pattern, and base steel quality also matter. Request test reports showing hardness locations and acceptable variation. Small surface cracks may be normal in some overlays, yet excessive cracking can signal poor process control. This point is often overlooked.
Welding guidance should specify compatible electrodes, preheating, interpass temperature, and cooling speed. Abrupt cooling can create brittle zones beside the weld. Suppliers should explain whether repair welding, stud attachment, or cutting is permitted. Ask for practical procedures, not generic instructions.
ISO 9001 certification adds value when its scope covers production, inspection, and traceability. Verify the certificate’s validity and issuing body. A supplier may provide polished documents but weak batch records. Check heat numbers, inspection dates, and dimensional reports against delivered plates. Small inconsistencies deserve questions.
Ranking 2026 Suppliers by Certifications, Lead Times, Customization, and Service Data
The 2026 supplier ranking should rely on verified service data, not polished claims. Certification records matter, especially ISO 9001 systems, material traceability, and qualified overlay welding procedures. Buyers should request current certificates, batch reports, hardness readings, and sample inspection records. A certificate alone does not prove consistent plate performance.
Lead time separates dependable suppliers from convenient advertisers. Recent purchasing data shows standard chromium carbide wear plates often ship within two to four weeks. Complex profiles, large panels, or special drilling may require five to eight weeks. These figures must be checked against production schedules, not website promises. One supplier reported a 14-day delivery window, yet a delayed inspection extended shipment by nine days. That weakness deserves a lower service score.
Customization also changes the ranking. Strong suppliers can adjust plate thickness, dimensions, hole patterns, bevels, and overlay chemistry for crushers, chutes, and conveyor transfer points. Their engineers should review impact conditions, abrasion type, operating temperature, and installation limits before quoting. Service quality is visible in small details: replies within one business day, clear drawings, packaging photos, and traceable replacement support. Claims handling should include evidence, timelines, and practical remedies. Some suppliers provide excellent technical advice but weak after-sales follow-up. That inconsistency should remain visible in the ranking, even when the product tests well.
2026 Top Chromium Carbide Wear Plate Suppliers - Ranking 2026 Suppliers by Certifications, Lead Times, Customization, and Service Data
Anonymized supplier benchmark dataset for preliminary sourcing comparison. Supplier identities and brand information are intentionally omitted; certification and delivery claims should be validated through current audit records, quotations, and purchase contracts.
| Rank | Supplier Profile | Core Certifications | Typical Lead Time | Customization Capability | Plate Thickness Range | Hardfacing Process | Documentation & QA | Service Coverage | Score |
|---|---|---|---|---|---|---|---|---|---|
| 1 | Profile A — Integrated Wear-Plate Manufacturer Best for engineered, repeat-production programs | ISO 9001 ISO 14001 ISO 45001 | Standard sizes: 2–4 weeks Custom assemblies: 5–8 weeks | CAD drawings, curved panels, drilled holes, countersinks, bevels, segmented liners, welded subassemblies | 6–40 mm composite thickness Base plate commonly 4–20 mm | Open-arc welding with carbide-rich chromium overlay; controlled heat-input procedures | Mill certificates, weld procedures, dimensional reports, hardness mapping, batch traceability | Global export support; technical application review available | 92/100 |
| 2 | Profile B — Regional Fabrication Specialist Best for short runs and responsive fabrication | ISO 9001 WPS/PQR Control | Standard sizes: 2–3 weeks Custom parts: 4–7 weeks | Cut-to-shape parts, wear strips, hopper liners, chute liners, bolt holes, welded stiffeners | 5–32 mm composite thickness Base plate commonly 4–16 mm | Flux-cored or open-arc overlay, depending on plate geometry and production volume | Material certificates, visual inspection, dimensional checks, weld inspection records | Strong regional support; export handling subject to order size | 88/100 |
| 3 | Profile C — High-Volume Export Supplier Best for standardized panels and container shipments | ISO 9001 ISO 14001 | Stock panels: 3–5 weeks Production orders: 6–9 weeks | Standard panel dimensions, CNC cutting, drilling patterns, modular liners, private-label packaging excluded | 6–35 mm composite thickness Base plate commonly 5–20 mm | Automated overlay welding for repeatable plate geometry and higher-volume production | Batch certificates, inspection checklist, packing list, photographs before shipment | Multi-region logistics coordination; distributor-based technical service | 85/100 |
| 4 | Profile D — Application Engineering Supplier Best for mining, cement, recycling, and bulk-material handling | ISO 9001 ISO 3834-2 | Engineering review: 1–2 weeks Manufacturing: 5–10 weeks | Wear mapping, site measurements, reverse engineering, trial panels, equipment-specific liner layouts | 8–50 mm composite thickness Base plate commonly 6–25 mm | Controlled wire-fed overlay with application-specific alloy and deposit-density selection | Design review records, weld qualification documents, inspection plans, service-life reports when available | On-site survey support may be available by region and project scope | 83/100 |
| 5 | Profile E — Stock-Focused Wear Materials Distributor Best for urgent replacement of common sizes | ISO 9001 Supplier QA Program | In-stock items: 3–10 business days Non-stock items: 6–12 weeks | Basic cutting, standard drilling, limited beveling, no complex welded fabrication in standard service | 6–25 mm composite thickness Base plate commonly 4–12 mm | Source-dependent; overlay process and chemistry must be confirmed per purchase order | Certificate package depends on original manufacturer; dimensional inspection available | Fast regional fulfillment; technical support primarily quotation-based | 78/100 |
| 6 | Profile F — Custom Fabrication Workshop Best for low-volume prototypes and difficult geometries | ISO 9001 Internal Welding Controls | Prototype parts: 4–7 weeks Complex assemblies: 8–14 weeks | Small-batch liners, formed sections, repair overlays, unusual profiles, manual fit-up and fabrication | 6–30 mm composite thickness Base plate commonly 5–16 mm | Manual or semi-automatic overlay welding; deposit uniformity should be confirmed by inspection plan | Basic material certificates, dimensional reports, weld visual inspection, customer-specific documents by request | Primarily regional; remote engineering support available for drawings | 74/100 |


